What should accompany a revised tube drawing?
State what changed and include the current section, material, wall thickness, stock length and quantity. Keep the new revision clearly identified.
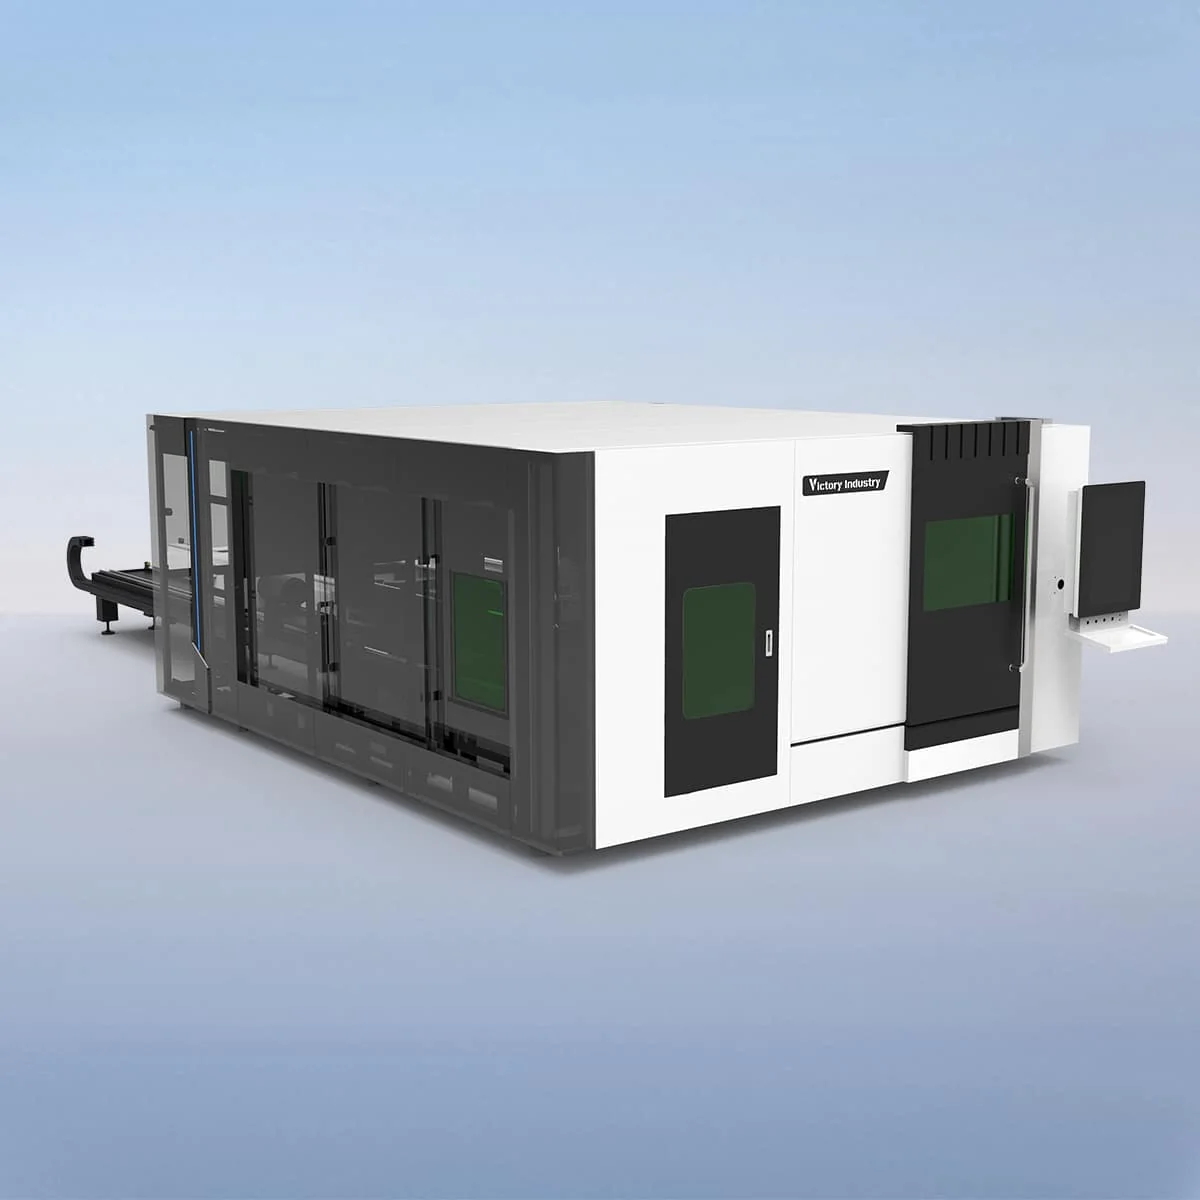
Tube And Sheet Laser Cutting Machine
VIP4015T tube application configuration should carry a record of what changed between the first inquiry and the current quotation. A revised tube drawing, different sheet stock and a new component preference are separate changes. Keeping them separate makes the proposed equipment easier to review against the work now required.
The VIP-T table lists VIP4015T at 4000*1500mm Cutting Area with a 1500-20000W power range. It is part of the tube and sheet range. Treat the area as a sheet reference; no tube diameter or loading-length specification can be assumed from that entry.
| Specification | VIP4015T |
|---|---|
| Cutting Area | 4000*1500mm |
| Laser Head | Raytools, WSX, BOCI, Osprey |
| Laser Power | 1500-20000W |
| Laser Generator | Raycus, MAX, IPG |
| Control System | CypCut, Weihong |
| Servo Motor And Driver | Fuji, Delta, Yaskawa |
| Guide Rails | Taiwan Linear Rails |
| Reducer | Japan Shinbo, France Mortori |
| Max. Acceleration | 1.3G |
| Max. Linkage Speed | 140m/min |
| Z Axis Travel | 300mm |
| Positioning Accuracy | 0.05mm |
| Repositioning Accuracy | 0.03mm |
Configuration options vary by model. Confirm the final specification, selected components and operating requirements with your quotation.
For a revised VIP4015T tube project brief, identify the current drawing and list the changed features or dimensions. Retain section shape, outside size, wall thickness, material and incoming length beside it. Include the required quantity so the supplier does not have to reconstruct the application from several earlier messages.
Record sheet-stock changes separately. VIP4020T lists 4000*2000mm compared with VIP4015T's 4000*1500mm. The first dimension stays the same while the second changes. Use this comparison where the revised sheet requirement calls for it, without implying that it answers a revised tube question.
VIP4015T lists 1.3G maximum acceleration, 140m/min Max. Linkage Speed and 300mm Z axis travel. The accuracy entries are 0.05mm Positioning Accuracy and 0.03mm Repositioning Accuracy. Preserve their names in the comparison; they do not establish material cutting time or compliance with a finished-part tolerance on the revised drawing.
VIP4015T machine options should be compared against one current application record. If the change is only to a sheet format, keep the tube description attached and unchanged. If the tube material or length changes, mark it explicitly instead of assuming an earlier discussion still answers the new requirement.
A revision record can be simple: identify the changed item, its former reference and the current requirement. Ask the offer to show which version it addresses. This is useful when a component change and a workpiece change occur together, because a different price does not explain which change caused it.
Keep questions about the proposed tube arrangement open until they receive a specific response. The sheet area cannot provide a tube-section or loading answer. Future work that has not yet been fully described should remain separate from the current equipment scope, even if it appears in the same conversation.
VIP4015T quotation requirements include a selected power within the published range. The head alternatives are Raytools, WSX, BOCI and Osprey; generators are Raycus, MAX and IPG; controls are CypCut or Weihong. Name the proposed combination and retain the quotation revision beside the relevant drawings.
The drive list contains Fuji, Delta and Yaskawa, with Taiwan Linear Rails and Japan Shinbo or France Mortori reducers. If any chosen component differs from an earlier offer, identify that difference explicitly. Do not compare a current selection with an earlier unselected list of alternatives as though they described identical equipment.
Request the current overall equipment dimensions, supplied-item scope and installation information for the destination. A sheet-area entry is not a layout drawing. Use the series and adjacent-model links to review published parameter differences, then submit the consolidated current requirements through the contact page.
State what changed and include the current section, material, wall thickness, stock length and quantity. Keep the new revision clearly identified.
It lists 4000*2000mm rather than VIP4015T's 4000*1500mm. The comparison changes the second area dimension.
Do not assume it does. Identify the changed length and ask for the proposed arrangement to be addressed against the current requirement.
Record the selected power, head, source, controls and drives in both offers, separately from changes to the workpiece information.
The 140m/min entry is Max. Linkage Speed. It is not evidence of a material cutting rate or a completed-part production target.
Compare VIP-T Laser Cutting Machine models
Share your material, dimensions and process. Start a conversation about the right configuration.